Capabilities
Capabilities
What we cut, bend, join and finish, with the limits that matter when you design. All figures are indicative for this concept.
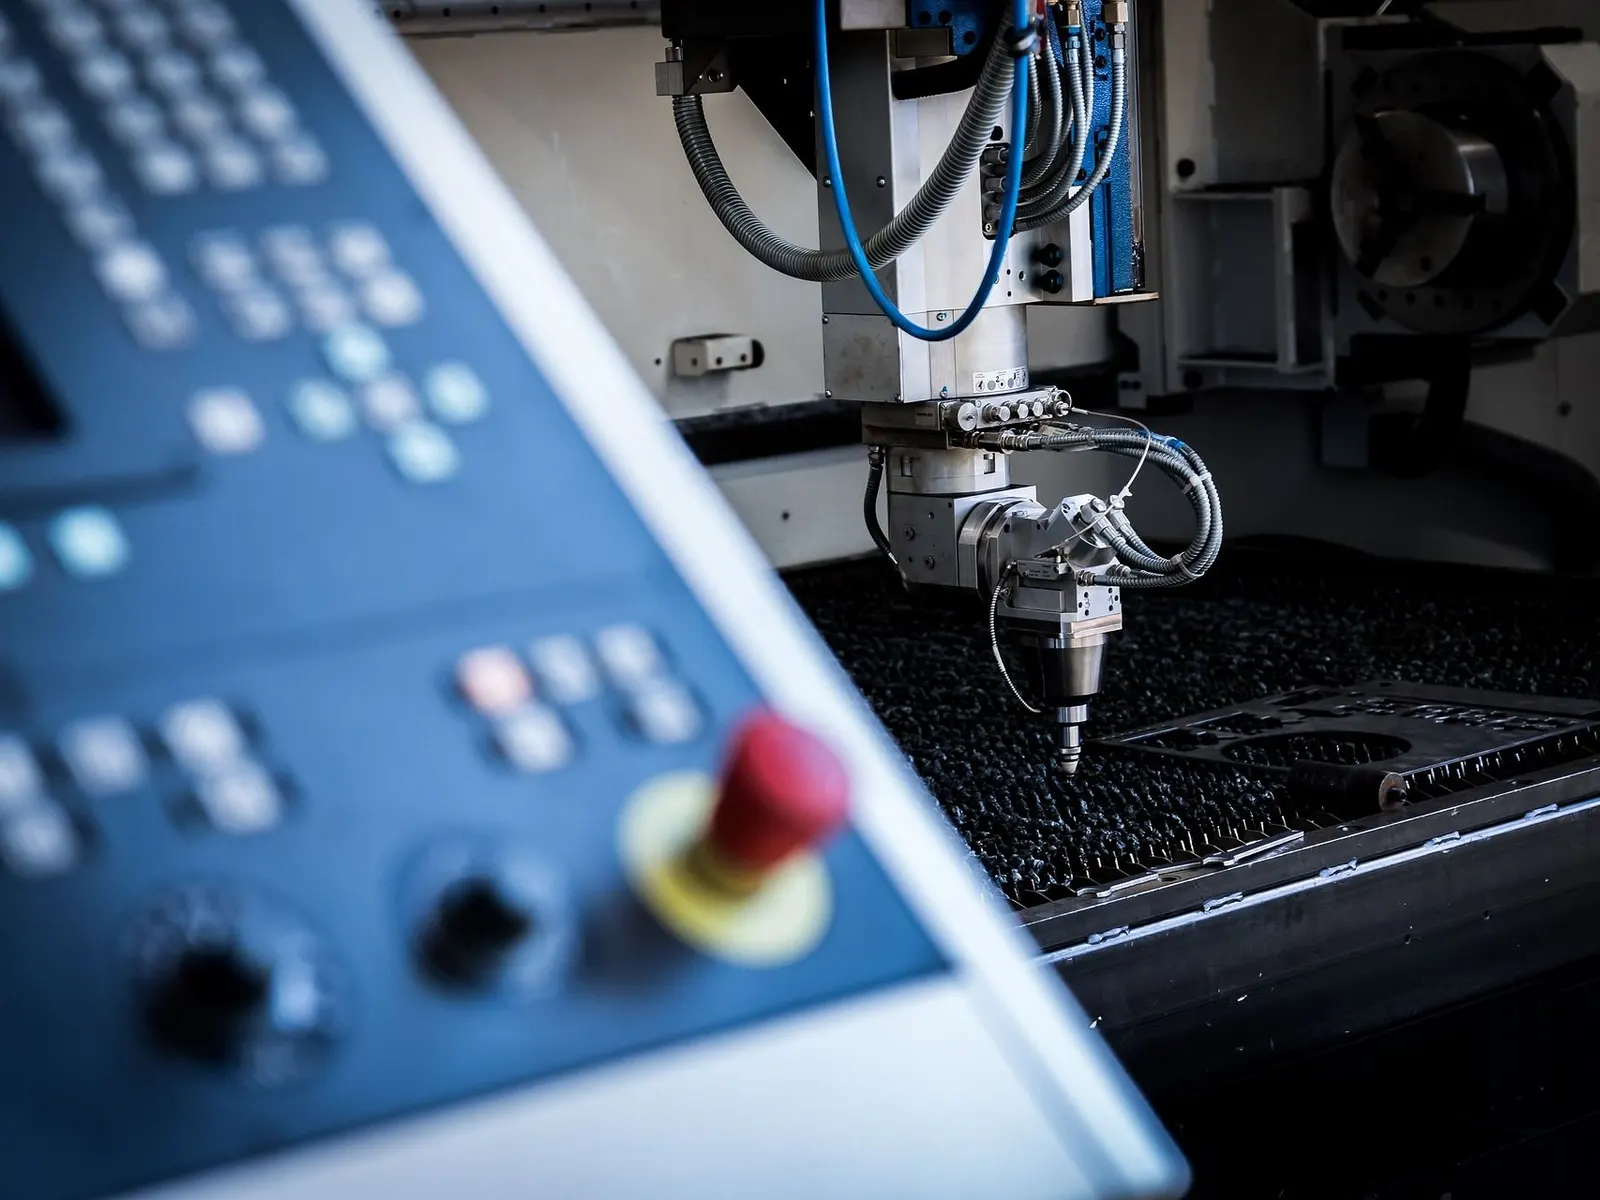
Machine limits
| Process | Max size | Thickness | Typical use | Added lead time* |
|---|---|---|---|---|
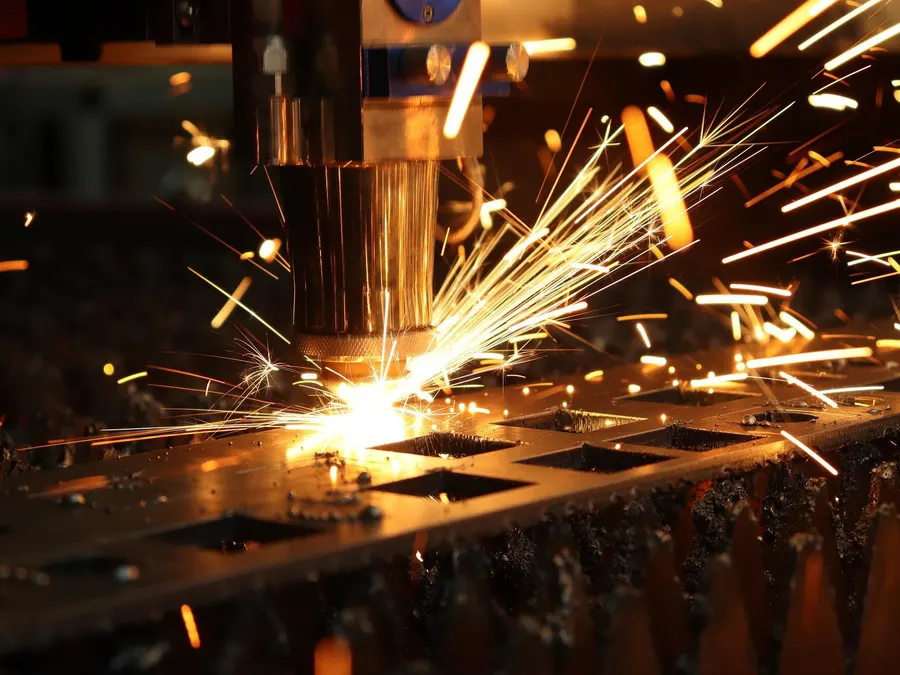
| Fibre laser cutting | 3000 × 1500 mm | steel ≤ 20 · SS ≤ 12 · Al ≤ 10 mm | Contours, holes, slots, engraving | base |
| CNC press brake | 3000 mm bend length | 0.5–12 mm | Flanges, hems, offsets, boxes | +1 day |
| Deburring / edge rounding | 1500 mm width | 1–20 mm | Safe edges, coating adhesion | included |
| Press-in fasteners | M3–M10 | ≥ 0.8 mm | Nuts, studs, standoffs | +1 day |
| TIG / MIG welding | 2000 × 1000 mm | ≥ 1 mm | Frames, closed boxes, brackets | +1–2 days |
| Powder coating | 2500 × 1200 × 1000 mm | — | RAL colours, fine structure | +2–3 days |
| Assembly & kitting | per agreement | — | Sub-assemblies, labelled kits | +1–3 days |
* On top of the agreed base lead time for cutting. In this concept, lead times are illustrations, not commitments.
Series
Built for 10 to 5,000 pieces
Below ten pieces, online platforms are often faster. Above a few thousand, dedicated tooling or stamping becomes interesting. In between, laser cutting and CNC bending stay flexible: no tooling cost, revisions without scrap, and stable batch prices with call-offs.
Call-off batches, buffer stock and kanban are agreed per part in a real engagement.
Who reads this page
Buyer
Max sizes, lead time additions and which steps stay under one roof.
Design engineer
Thickness ranges and where to find tolerances: laser cutting & bending.
Start an RFQ